Featured OEM Products & Storage Solutions
Precision-manufactured commercial fitness infrastructure, high-density plate trees, strength units, and shock-absorbent flooring engineered for global commercial facilities.
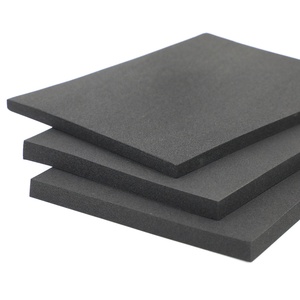
1000*1000 Rubber Gym Floor Tiles for Fitness
Get a Quote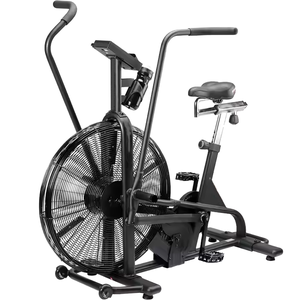
High Quality Commercial Indoor Air Bike Exercise Wheel Wind Resistance Spinning Bike
Get a Quote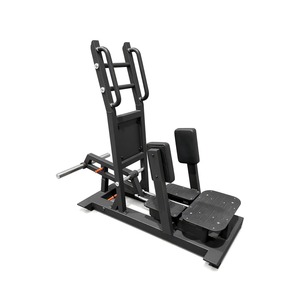
Commercial Use Gym Plate Loaded Hip Thrust Machine Glute Drive
Get a Quote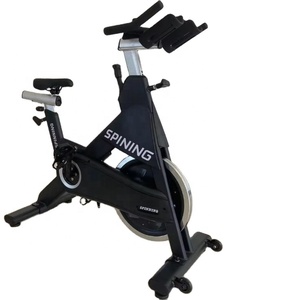
Fitness Commercial Spinning Bike Heavy-Duty Gym Exercise Cycle
Get a Quote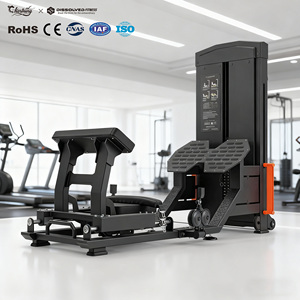
DISSOLVED Strength Machine Leg Extension Curl Hip Lift Thrust Full Set
Get a Quote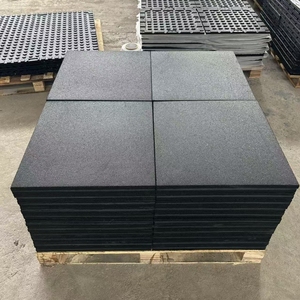
Guangdong Factory Matt Top Gym Rubber Flooring Shock Absorption Anti-Slip Tile
Get a Quote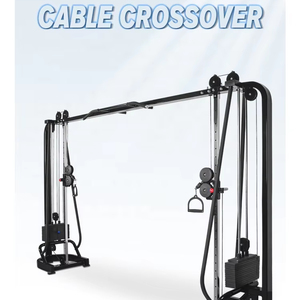
Hot Sale Commercial Cable Crossover Strength Training Station
Get a Quote
Professional Heavy Duty Adjustable Weight Bench Dumbbell Fitness Chair
Get a QuoteWhy Commercial Procurement Leaders Partner with Our OEM/ODM Infrastructure
Designed with engineering roots in California and supported through strategic logistics hubs in Miami, Florida, USA, our manufacturing ecosystem serves commercial gym operators, franchise networks, and fitness distributors across more than 60 countries.
One Integrated Range
From weight plate trees and storage racks to plate-loaded strength lines, selectorized machines, cardio, and rubber flooring—specify your entire floor with unified visual design and laser-fit tolerances.
Biomechanically & Structurally Engineered
Developed around stress-distribution mechanics. Heavy-duty 11-gauge Q235B/Q355B structural steel tubing welded under automated robotic MIG systems ensures absolute structural rigidity under 1,500+ lbs of continuous load.
Built to Your Brand (Full OEM Customization)
Custom powder coating finishes (electrostatic micro-texture or high-gloss), laser-cut brand endcaps, stainless steel peg sleeves, and custom color-matched polyurethane protective bumpers specified at factory-direct level.
Complete Procurement Documentation
Speed up facility layout and structural engineering sign-offs with direct access to 2D/3D CAD models, spec sheets, BIM objects, pre-installation floor surveys, and comprehensive factory warranty coverage.
Engineering Whitepaper: Structural Optimization & OEM Sourcing Standards for Weight Plate Storage Infrastructure
In high-traffic commercial fitness centers, strength training facilities, and university athletic complexes, weight plate storage units—commonly designated as weight plate trees, bumper plate racks, or Olympic plate tree towers—serve as critical operational bottlenecks. While frequently categorized as static utility furniture, the structural integrity, peg angle geometry, center-of-gravity stabilization, and surface abrasion resistance of weight trees directly influence facility safety, floor longevity, and member workout efficiency.
1. Metallurgical Selection & Load-Bearing Physics
Low-grade commercial weight trees manufactured from 1.5mm to 2.0mm thin-wall tubing routinely suffer from structural shear at weld junctions when fully loaded with bumper plates exceeding 1,000 lbs (450 kg). Premier OEM/ODM suppliers utilize heavy-gauge carbon steel structural tubing engineered to withstand extreme static load vectors:
- Structural Frame Tubing: Premium Q235B or high-tensile Q355B steel, featuring 50x75mm, 60x60mm, or 50x100mm profile dimensions with wall thicknesses of 2.5mm to 3.0mm (11-Gauge).
- Weight Storage Peg Construction: Solid steel bar stock or cold-drawn thick-wall steel pipe (minimum 48mm outer diameter) wrapped in hard-chrome, stainless steel, or high-density thermoplastic polyurethane (TPU) sleeves to prevent metal-to-metal scraping and oxidation.
- Base Frame Geometry & Tipping Moment Arm: A triangular or A-frame wide-base structure engineered with a minimum base footprint ratio of 1:1.4 relative to total height. This lowers the center of gravity and ensures a static tip-over angle threshold of ≥18 degrees even when upper storage horns are unevenly loaded.
| Material Specification | Standard Commercial Grade | OEM Heavy-Duty Commercial (Skelcore Standard) | Impact on Facility Operational TCO |
|---|---|---|---|
| Steel Wall Thickness | 1.5mm – 2.0mm (14-16 Gauge) | 2.75mm – 3.0mm (11 Gauge) | Eliminates frame flex, tube buckling, and weld fatigue failure. |
| Storage Horn Protection | Bare Painted Steel / Soft PVC Cap | Stainless Steel Sleeve / TPU Shield + Urethane Bumpers | Prevents rust spots, paint flaking, and bumper plate core damage. |
| Welding Protocol | Manual Spot Welding | Full-Seam Robotic MIG Welding | 100% structural uniformity across multi-axis joint intersections. |
| Finishing Technology | Single-Layer Solvent Paint | Dual-Coat Electrostatic Zinc Primer + Thermosetting Powder | Passes 800-Hour Salt Spray Corrosion Resistance Testing. |
2. Ergonomic Horn Spacing & Bumper Plate Compatibility
Modern commercial gyms have largely transitioned from traditional thin iron plates to thick high-density rubber bumper plates (IWF standard 450mm outer diameter) and wide-flange urethane plates. Traditional weight tree designs frequently fail because storage horns are positioned too closely, rendering half the storage pegs unusable.
Engineered OEM manufacturing requires rigorous horizontal and vertical horn offset design:
- Vertical Horn Clearance: Minimum 470mm clear spacing between vertical storage tiers to allow simultaneous storage of standard 450mm bumper plates across all levels without plate overlapping.
- Horizontal Horn Angle: Storage pegs constructed with a 2 to 5-degree upward incline to prevent plates from creeping off during floor vibration or accidental bumps.
- Integrated Barbell Holders: Dual vertical 51mm sleeve receiver tubes welded directly to the base frame, lined with UHMW polyethylene liners to store two 20kg Olympic barbells vertically without damaging knurling.
Future Procurement & Manufacturing Trends (2025–2030)
How smart technology, modular design, and sustainable manufacturing are transforming commercial weight tree production for international B2B buyers.
Modular Add-On Ecosystems
Future OEM weight tree platforms are shifting from static single-purpose racks to modular strength hubs. Factories are standardizing laser-cut 50mm/75mm hole patterns along the central column, allowing operators to attach resistance band pegs, landmine sleeves, kettlebell trays, and dip station handles.
Smart Inventory & RFID Tracking
High-end commercial gym networks are demanding weight trees integrated with optical or RFID sensors beneath each storage peg. These sensors relay real-time weight utilization analytics to facility management software, alerting staff when free-weight zones are unorganized or missing plates.
High-Density Knock-Down (KD) Packaging
With global ocean freight costs fluctuating, OEM suppliers are re-engineering fully-welded frame structures into precision-interlocking Knocked-Down (KD) assemblies. Utilizing internal laser-cut sleeve connectors and grade 8.8 structural bolts, KD packaging reduces shipping volume by up to 65% without sacrificing end-user stability.
Laser Customization & Brand Cohesion
Stand out in a competitive fitness market with factory-direct OEM custom branding options. We provide CNC laser-cut logo plates, custom color-matched thermosetting powder coats, branded rubber endcaps, and custom laser-etched weight capacity indicators on each individual peg level.
Strict Quality Control & Load Certification
Every batch of OEM weight plate trees undergoes rigorous factory verification, including 48-hour static overload testing (loaded to 150% maximum rated capacity), drop-impact vibration analysis, 800-hour salt spray corrosion testing, and 3D coordinate measurement for perfect bolt alignment.
Frequently Asked Questions for Sourcing Directors
Clear answers to technical, logistical, and OEM manufacturing questions regarding weight plate tree procurement.
Q: What is the standard Minimum Order Quantity (MOQ) for custom OEM weight plate trees?
For standard production finishes with custom branding, our typical MOQ starts at 50 units. For full structural modifications or unique footprint CAD designs, factory MOQs generally range from 100 to 200 units. Combined full-container load (FCL) orders mixed with other strength equipment, benches, or racks qualify for flexible volume pricing.
Q: How do your factories prevent scratch marks and rust on weight tree pegs?
We eliminate raw painted weight pegs, which are prone to chipping. Instead, our commercial weight trees feature hard-chrome plated steel sleeves, 304-grade stainless steel sleeves, or high-density thermoplastic polyurethane (TPU) covers, backed by heavy-duty rubber bumper stops at the base of each peg to absorb plate impact.
Q: Are your weight trees designed to accommodate full-size IWF/IPF Bumper Plates?
Yes. All standard and custom OEM weight tree configurations are engineered with vertical horn clearances exceeding 470mm. This guarantees that standard 450mm diameter bumper plates can be loaded on all levels simultaneously without touching adjacent plates.
Q: What engineering documentation is provided for facility floor planning?
We supply complete technical packages for architects, gym designers, and procurement managers, including 2D floorplan dimensions, 3D STEP/CAD files, BIM objects, structural static load certificates, product manuals, and pre-installation assembly guides.
Q: What is the typical lead time for custom OEM manufacturing and global delivery?
Prototype engineering and sample validation typically take 15 to 20 days. Full OEM production cycles generally require 30 to 45 days post-sample approval. Global logistics coordination is handled seamlessly via sea freight (FCL/LCL) or door-to-door DDP shipment from our manufacturing bases and Miami distribution center.
Q: Can weight tree frames be customized to match existing gym equipment color schemes?
Absolutely. Our automated electrostatic powder-coating lines support full RAL spectrum color matching. Whether your facility requires matte velvet black, high-gloss silver, bright crimson red, or custom textured finishes, we formulate powder blends to match your exact brand identity specifications.
Partner with a Leading OEM Commercial Gym Equipment Factory
Upgrade your product lineup or equip your global facility network with biomechanically designed, heavy-duty weight plate trees and commercial strength infrastructure.
Get a Quote